
The following are detailed winding methods and precautions:
Preparation:
Material Selection: Select appropriate enameled wire (e.g., high-temperature resistant grade 155 or 180) according to the motor power and voltage level. The wire diameter error must be controlled within ±0.02mm.
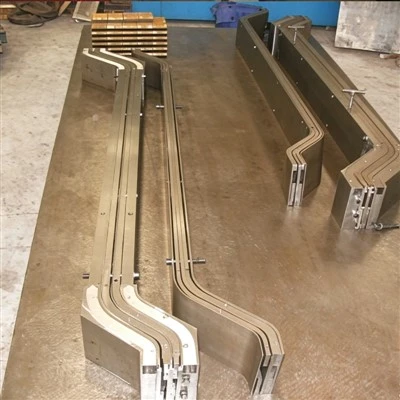
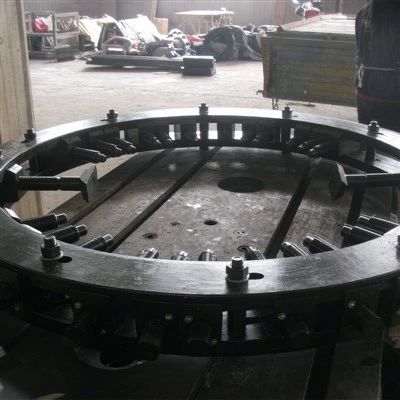
Die Calibration: The winding die must match the rotor core slot, with a gap not exceeding 0.1mm to prevent loosening during winding.
Winding Steps:
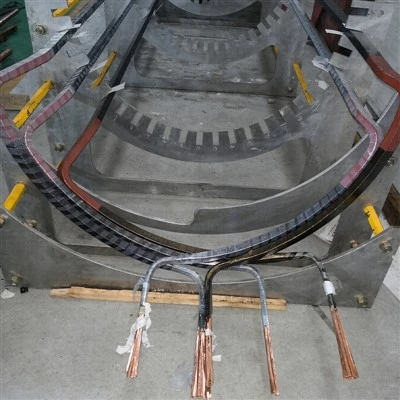
Starting Winding and Positioning: Begin winding from the starting slot of the rotor core, leaving a 10-15cm wire end for subsequent welding.
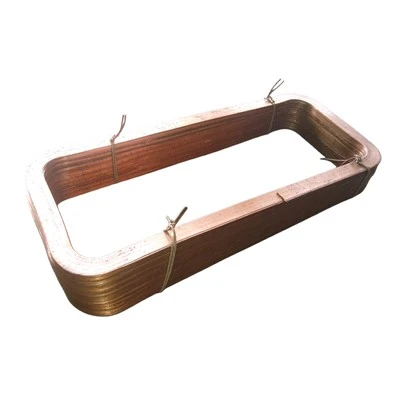
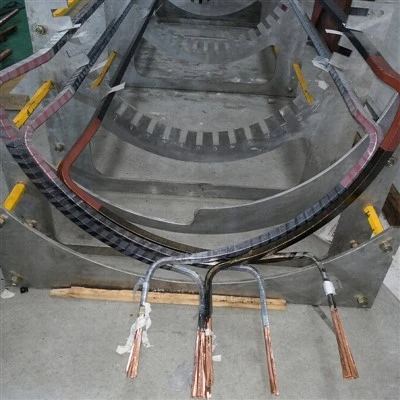
Layered Winding: Use the "overlapping winding method" or "wave winding method." Each layer of winding must be tightly arranged, with 0.05mm insulating paper between layers. The number of turns should not exceed ±2 turns.
Tension Control: Set the winding machine tension to 1.5-2.5N. Too high a tension will cause damage to the enamel film, while too low a tension will result in loose winding.
Finishing Procedures:
End Binding: Bind the end coils with non-woven tape, using a binding torque of 3-5 kg·cm to prevent deformation due to centrifugal force.
Insulation Testing: After winding, test the insulation resistance with a 500V megohmmeter. It must be ≥100MΩ (at room temperature).